
Leaderboard
-
chestikoph1
Regular Member1Points296Posts

Popular Content
Showing content with the highest reputation on 10/23/18 in all areas
-
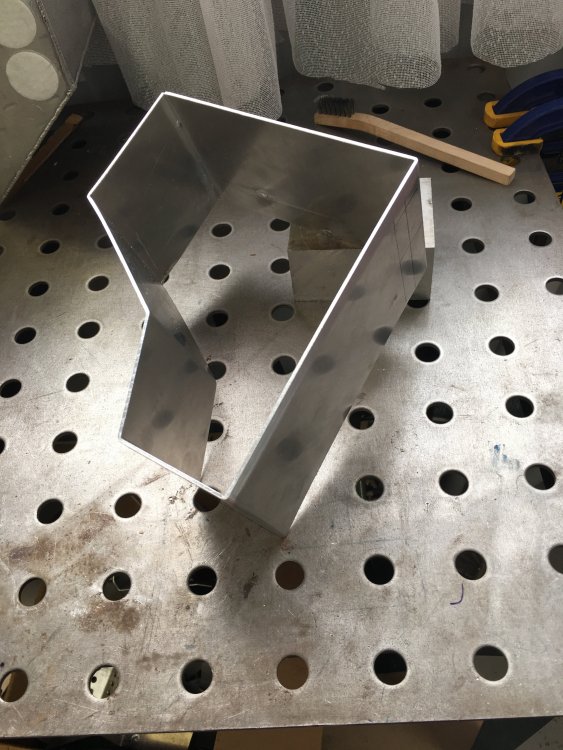
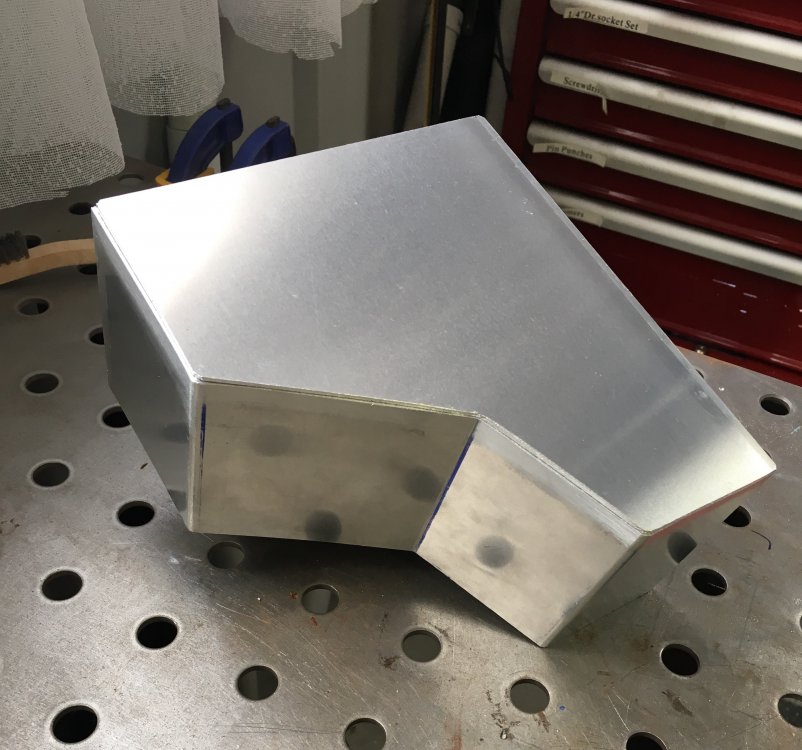
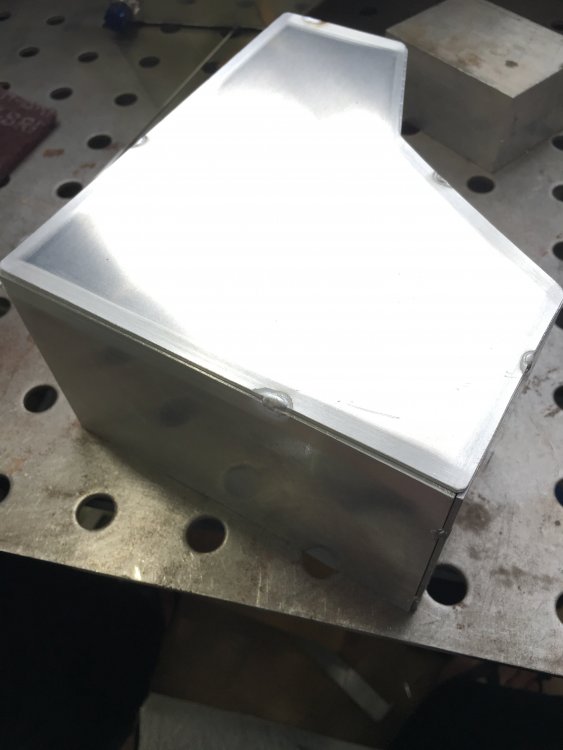
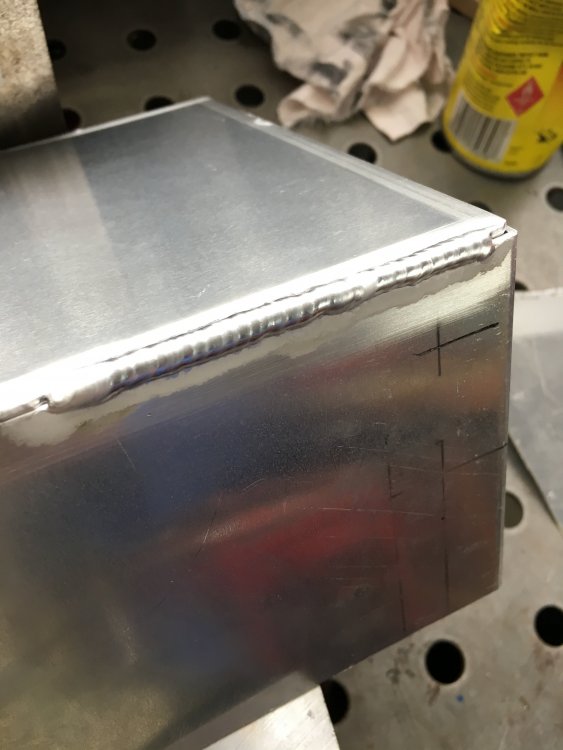
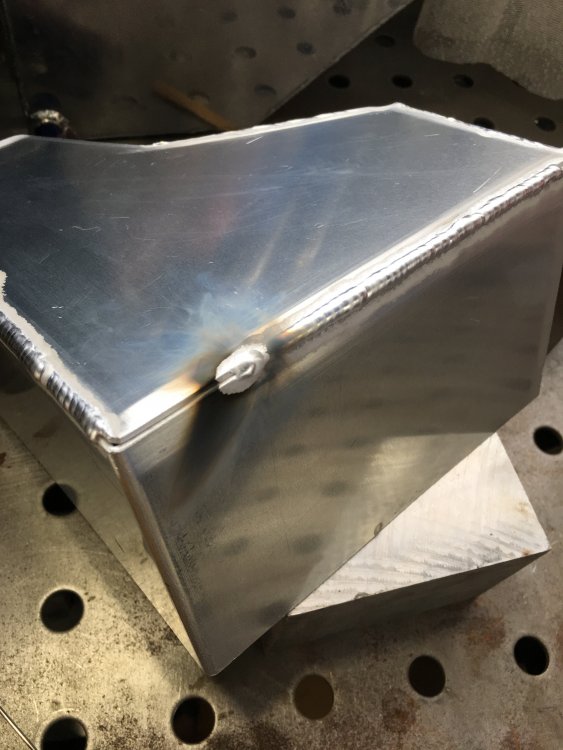
1 pointBefore i started the latest rebuild of the race car I bought myself a small AC/DC 180amp Tig welder, through out the build I knew I would requiring some Tig welding for some stainless and aluminium fabrication. I was sick of paying I stupid money for even the smallest of welding jobs, it seems like anytime a fabricator whips out the welder its a minimum $100 even for a 2 minute job. Anyway this post is about the fabrication of a custom catch can, now my Tig DC welding skills are average at best and my AC ally skills are crap, but after a bit of practice I was ready to try and fab myself a catch can. I used 2mm ally sheet, cut out using a jigsaw and bent up with a pan brake. I have found I got way better results when the fit up is perfect, you could almost fusion weld if there is no gap. Tacked the main box and one side... Once each side had a tack on it and I was happy with the positioning I started to weld it up, I welded about 3 inches at a time alternating sides. Ally gets hot really quickly and retains heat a lot more than steel and I don't have foot pedal to able to adjust the amps on the fly. This is what happens when you dab you tungsten in your weld pool, I tend to do this a lot, a pain in the ass, you have to clean your work and resharpen the tungsten.
 1 point


